

This case combines a buyer RFQ and drawing package with factory surface-treatment footage and packing/loading records for a Mauritius 132 kV transmission-line project scope reported at approximately 33 metric tonnes. The technical bill of materials required M20 property-class 8.8 bolts with matching class 8 nuts and spring washers, plus separate M12–M24 spring washers.
Customer identity, commercial terms and original drawings are not published. The 33-tonne figure comes from the working project/packing record supplied for this article; the buyer RFQ establishes the technical quantities and requirements, not a public final gross-weight or delivery certificate. Approved order documents, drawings and batch inspection records remain controlling.
Why the project required a controlled HDG fastener package
The procurement specification described a humid, saline tropical and cyclone-exposed service environment. It listed relative humidity above 95%, a 5–50°C ambient range and very heavy pollution conditions. These were project design inputs—not a claim that a generic bolt automatically meets every coastal application.
For this reason, the coating specification, thread allowance, post-galvanizing nut fit, inspection documents and export packing had to be reviewed together. Coating selection cannot be reduced to colour or a single catalogue phrase.
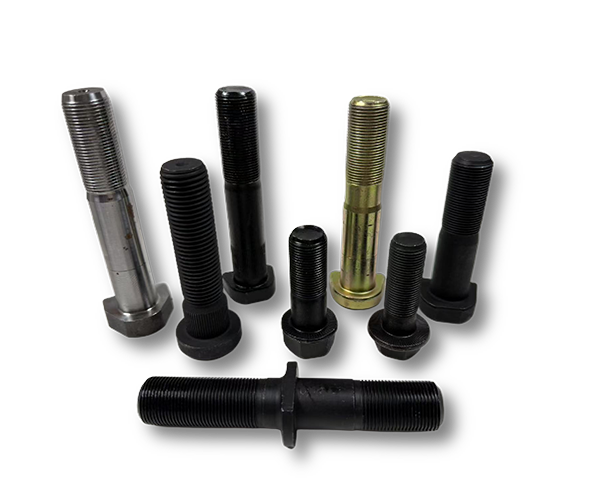
Project bolt and washer schedule
The project requirement covered 75,000 M20 bolt assemblies. Each set comprised one bolt, one matching nut and one M20 spring washer. Full-thread and partially threaded lengths were controlled by the drawings.
| Assembly size | Drawing thread requirement | Project quantity |
|---|---|---|
| M20 × 50 | Full thread | 10,000 sets |
| M20 × 55 | Full thread | 7,500 sets |
| M20 × 60 | Full thread | 7,500 sets |
| M20 × 65 | 26 mm thread | 7,500 sets |
| M20 × 70 | 28 mm thread | 7,500 sets |
| M20 × 75 | 30 mm thread | 7,500 sets |
| M20 × 80 | 32 mm thread | 7,500 sets |
| M20 × 90 | 36 mm thread | 10,000 sets |
| M20 × 100 | 40 mm thread | 10,000 sets |
An additional 35,000 hot-dip galvanized spring washers were specified: M12 (5,000), M14 (2,500), M16 (10,000), M18 (5,000), M20 (7,500) and M24 (5,000).
Drawing review and dimensional control
All M20 assemblies used a 30 mm bolt-head width across flats, 12.5 mm head height, 30 mm nut width across flats and 16 mm nut height. The matching M20 spring washer dimensions in the project drawing were 20.2 mm inside diameter, 33.6 mm outside diameter and 4.0 mm thickness.
The customer specification did not prefill the thread pitch; it required the supplier to declare the offered pitch. That point had to be closed during technical review instead of being assumed from the nominal diameter.
Standards, material and heat-treatment plan
The buyer RFQ referenced ISO 4017 for fully threaded hexagon bolts, ISO 4014 for partially threaded hexagon bolts, ISO 4032 for nuts, ISO 898-1 and ISO 898-2 for mechanical properties, ISO 965 for metric thread tolerances and ISO 10684 for hot-dip galvanized fasteners. The drawing-specific partial thread lengths were custom values and therefore required an approved written deviation instead of being presented as standard ISO 4014 dimensions. Spring-washer geometry was controlled by the approved project drawing; its product standard and test method required confirmation during technical review. For threaded fasteners, ISO 10684 was the primary HDG reference; ISO 1461 applied only where the project specification explicitly incorporated an applicable requirement. An ISO 9001 quality-management system was also requested.
- Bolts: heat-treated medium-carbon steel specified as property class 8.8. Final M20 mechanical acceptance values had to be reconciled with the approved ISO 898-1 requirement before production and inspection.
- Nuts: heat-treated medium-carbon steel, nut class 8, with geometry and mechanical properties controlled by the agreed standards.
- Spring washers: heat-treated medium-carbon steel to the project drawing and specification.
No unverified steel grade is published for this case. Material chemistry, heat-treatment route and lot traceability should be tied to the actual material certificate and inspection file.
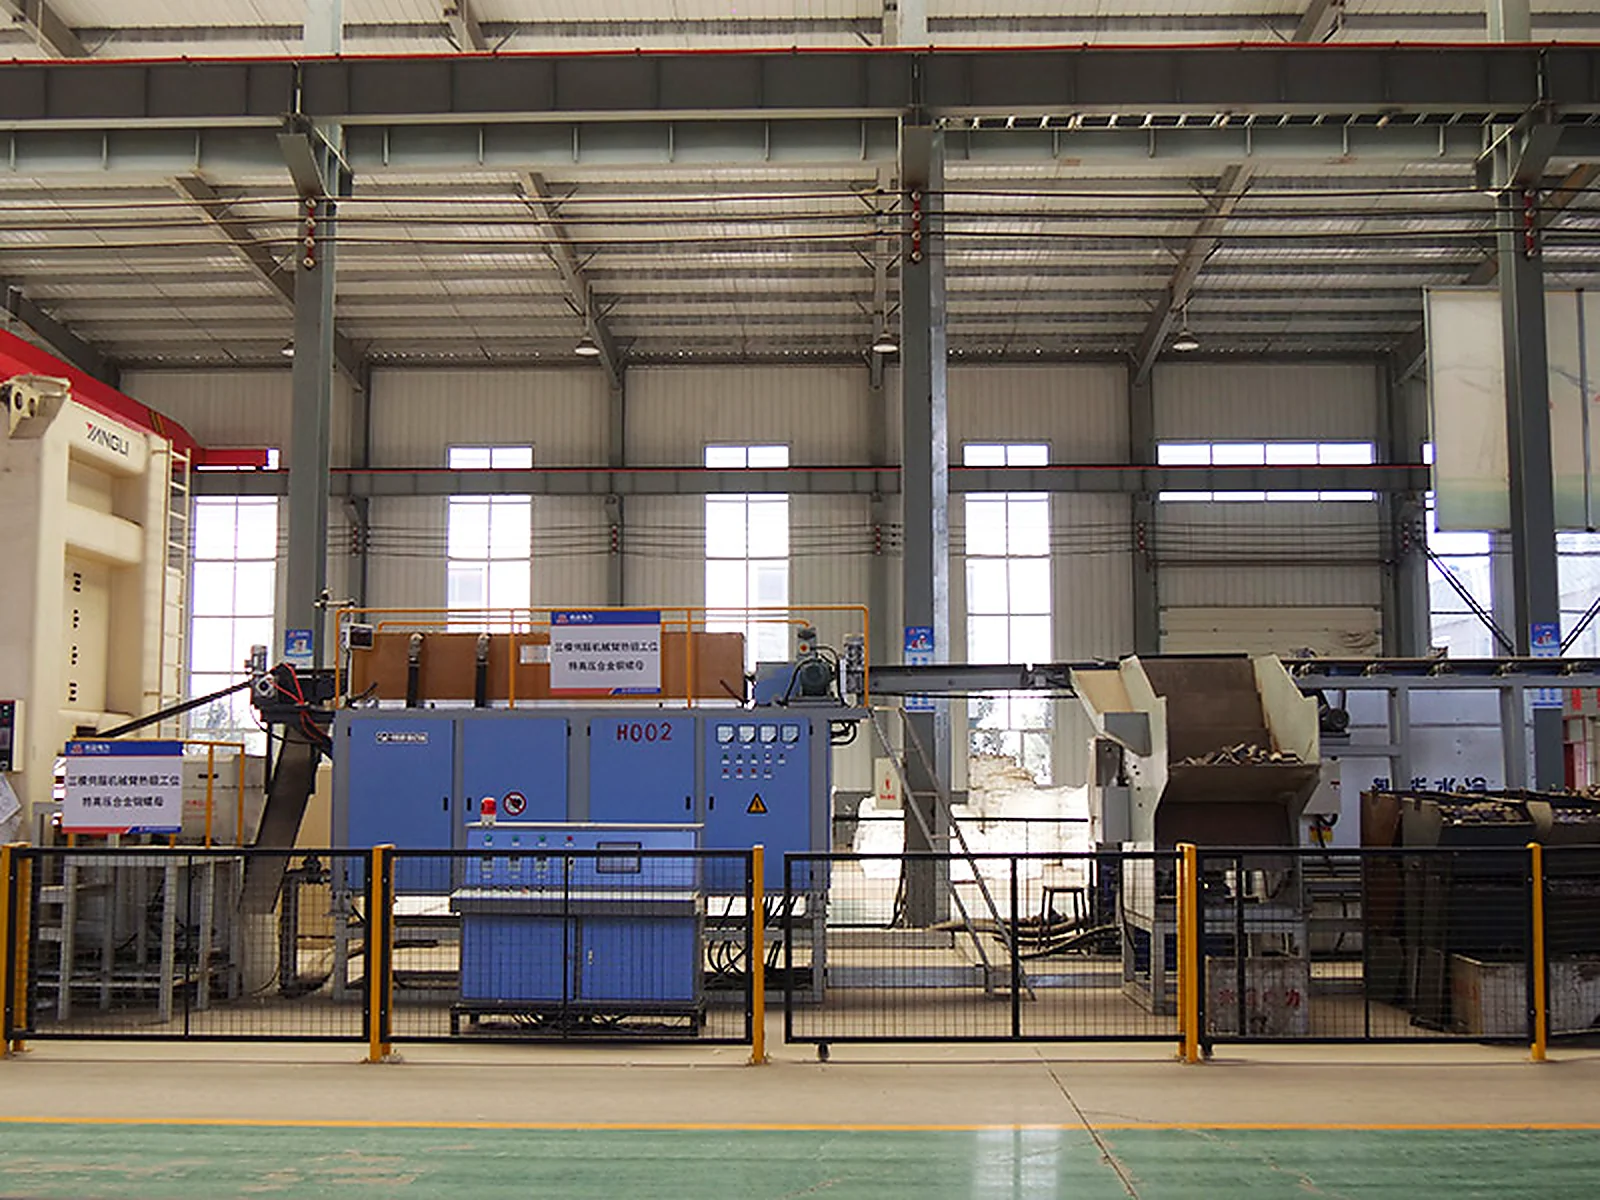
Hot-dip galvanizing and thread-fit control
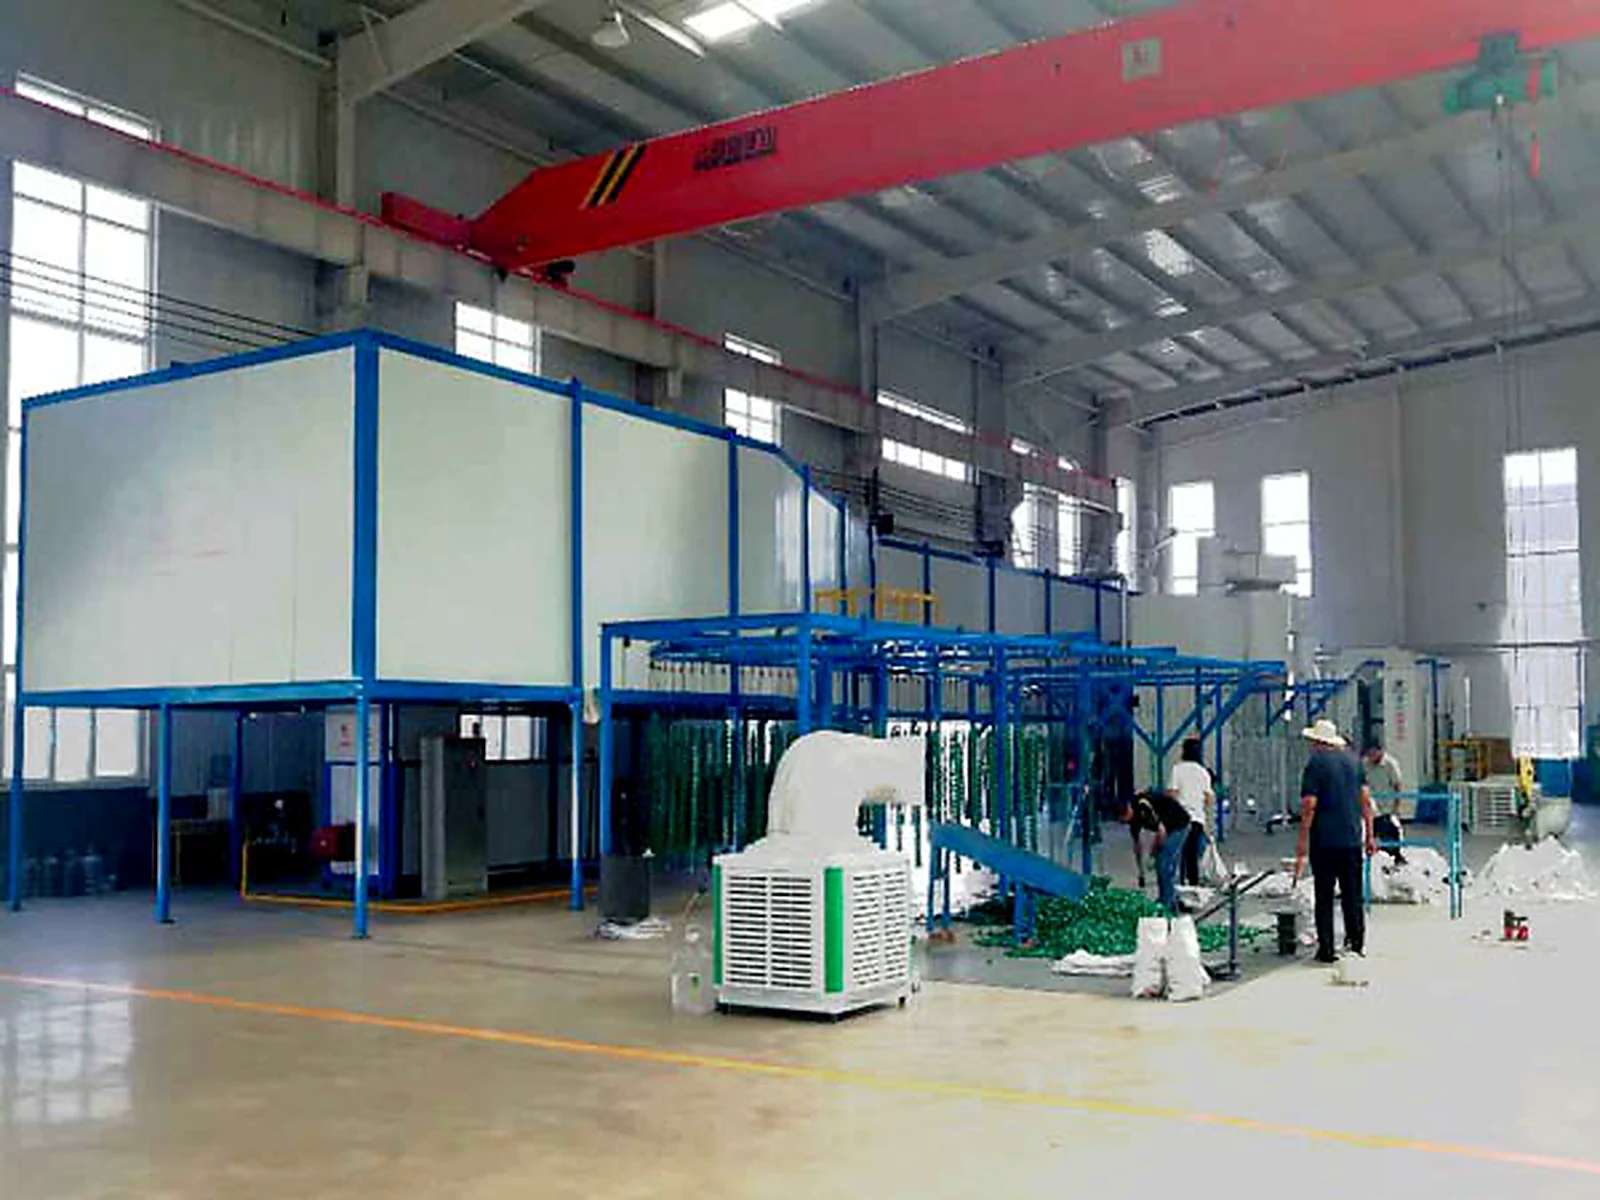
The technical file required bolts and nuts to be hot-dip galvanized after manufacture and threading; spring washers were to be galvanized after manufacture. The critical purchasing point was not only zinc coverage: the finished bolt and nut had to assemble normally without damaging the coating or thread. The project specification required galvanizing-conformity documentation and normal bolt-nut assembly.
The source documents did not state a public project-specific zinc-thickness value, so this case does not invent one. Coating thickness, sampling and acceptance values must be taken from the signed order, applicable standard and actual inspection report.
Inspection and document package
The project specification required an inspection and document package before dispatch. It requested dimensional and thread-fit verification, proof-load verification for bolts and nuts, material chemical-composition documentation, galvanizing conformity documentation and routine inspection records. The RFQ also listed a washer proof-load item; its test method and acceptance criteria required written clarification in the approved inspection plan.
- Verify each length and full-thread/partial-thread configuration against the approved drawing.
- Check bolt/nut mating after galvanizing; segregate and clearly label each item size.
- Record material, mechanical-property and coating documents requested in the purchase specification.
- Confirm any buyer or third-party witness inspection before dispatch.
This article describes the required control plan; it does not replace the batch-specific certificates or report measured test results that have not been approved for public release.
Export packing and container-loading record
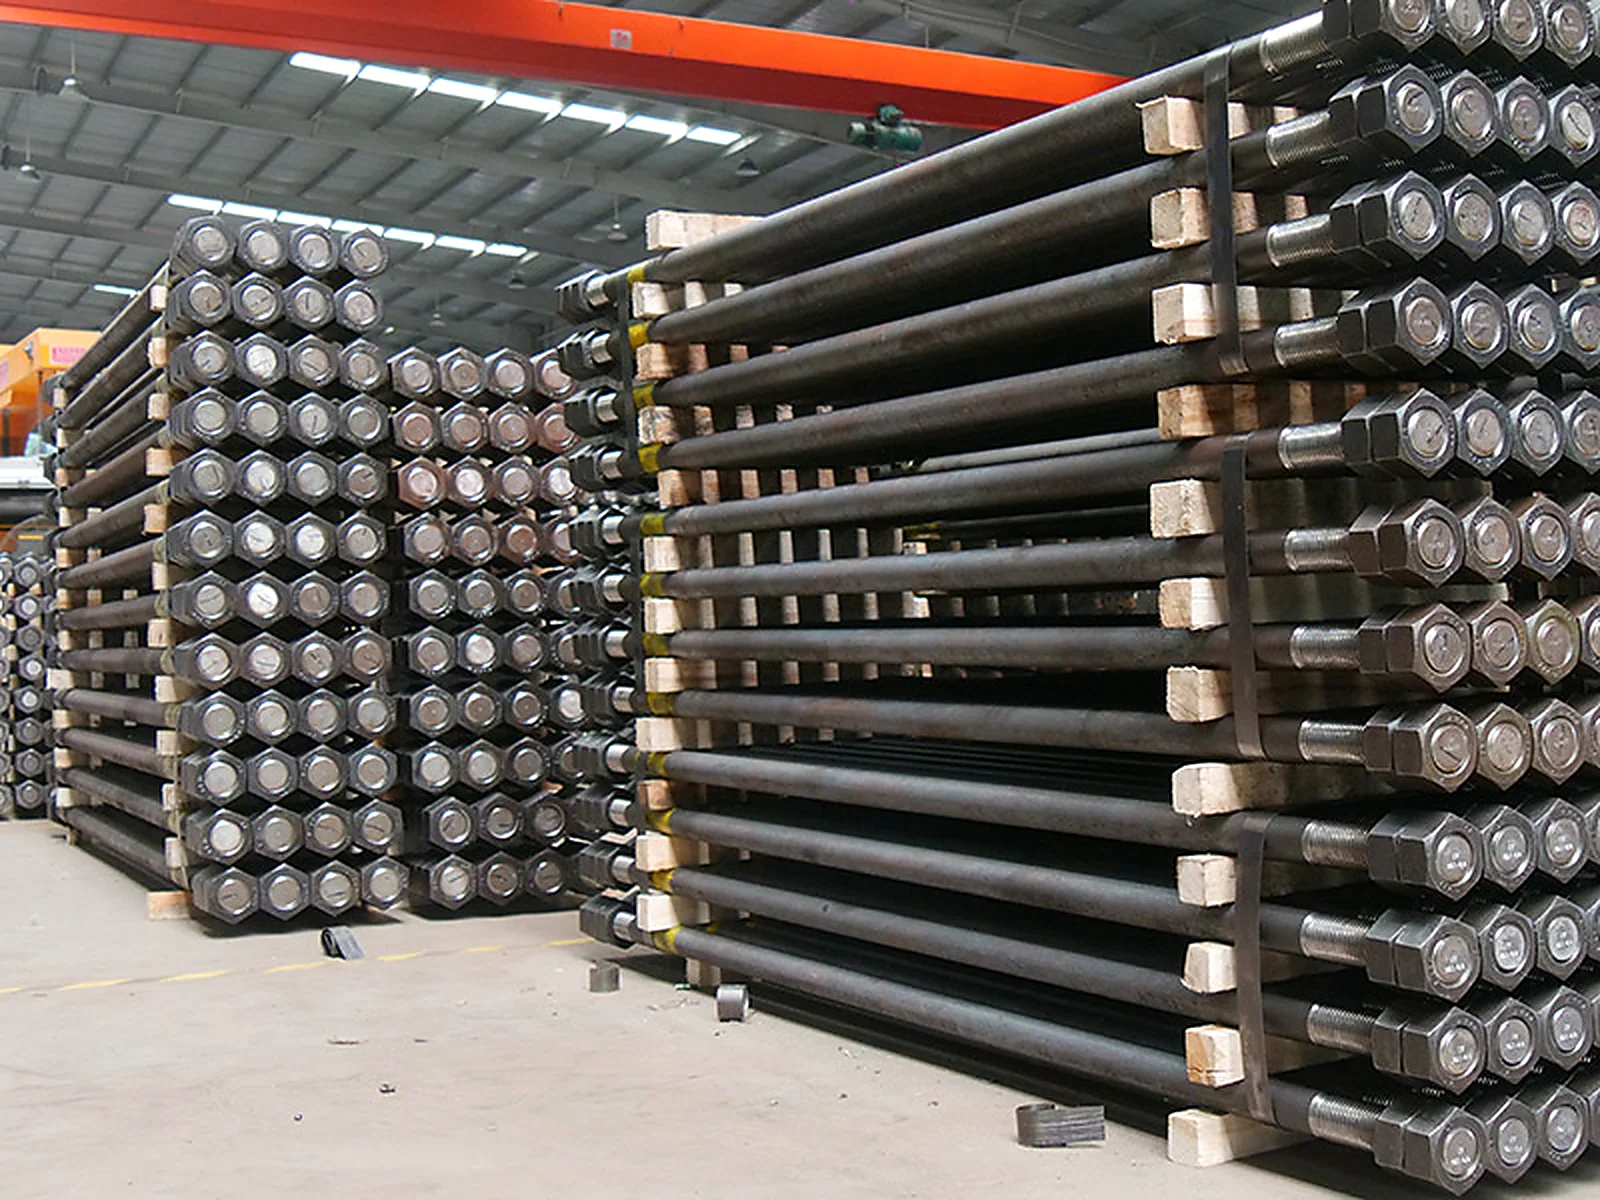
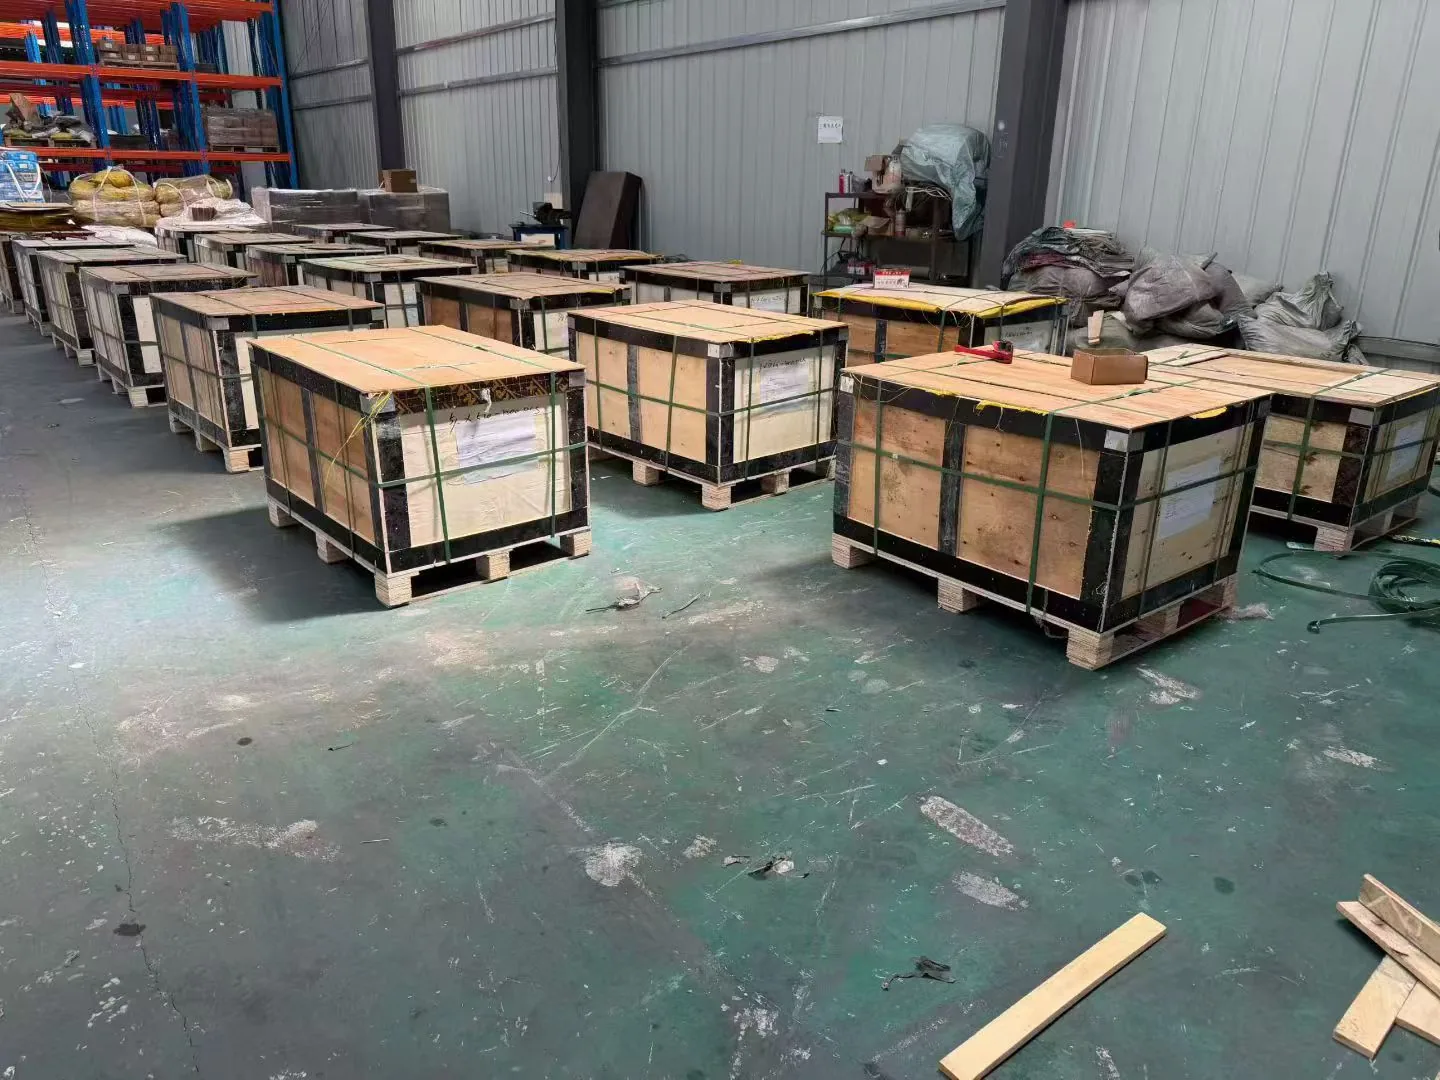
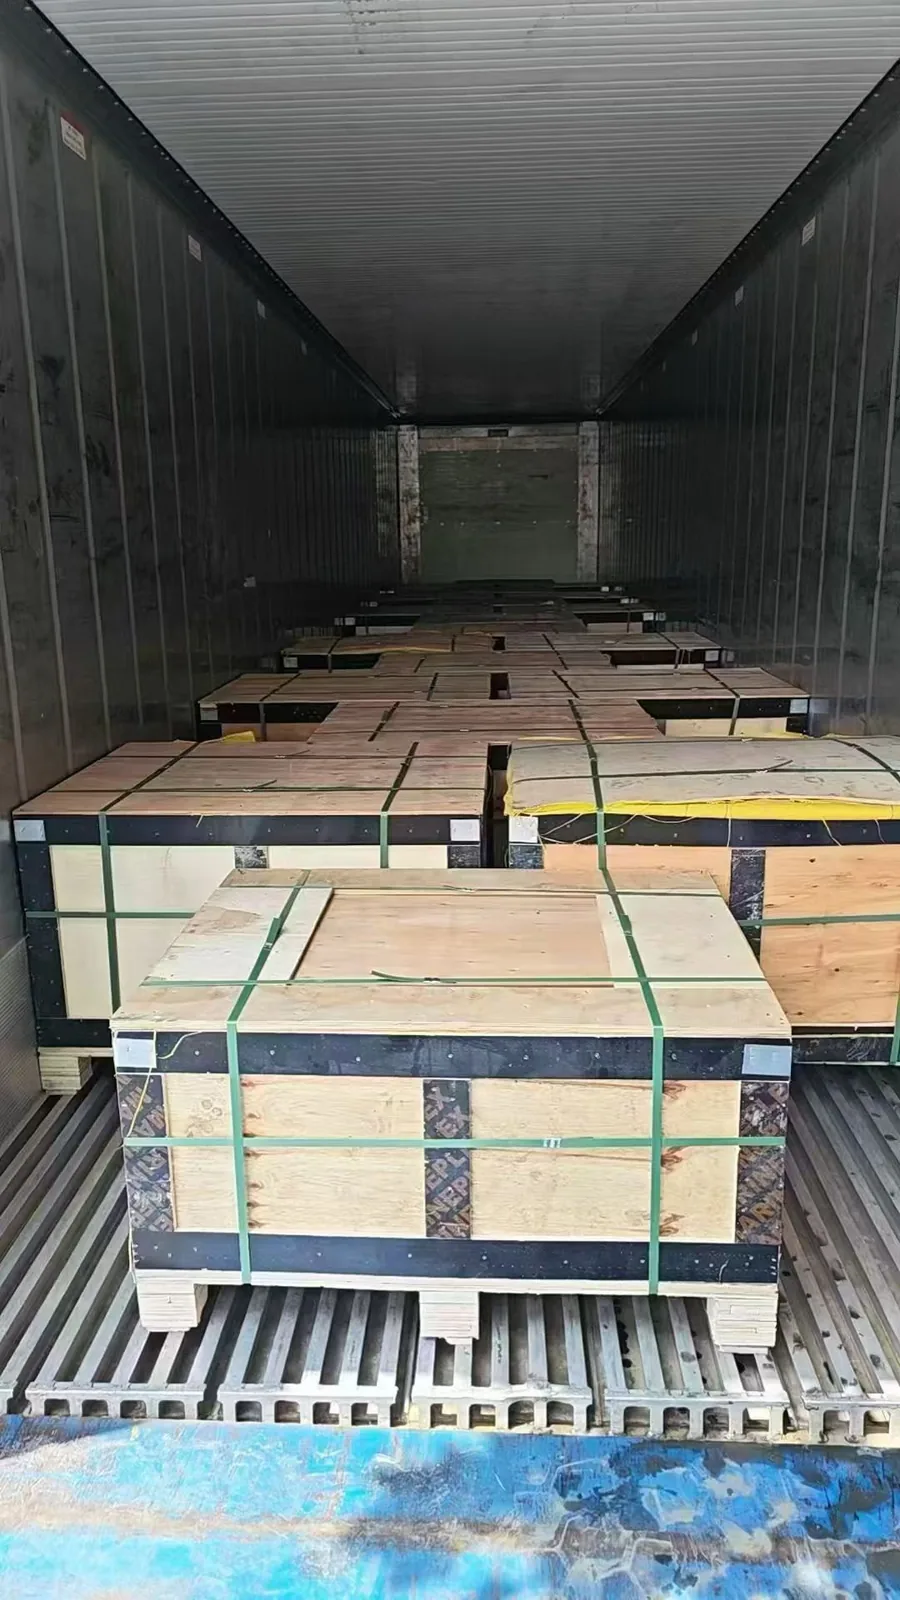
The working project record describes an approximately 33-tonne packing/loading scope separated by size and placed in reinforced export crates. The packing plan addressed high humidity, saline air, repeated handling and temporary storage. Package labels linked the product description, size and quantity to the packing list.
What buyers should send for a similar custom HDG bolt inquiry
- Project drawing and revision, or the exact current product standard
- Diameter, length, thread pitch, thread length and tolerances
- Material and property class for bolts, nuts and washers
- Hot-dip galvanizing standard, coating acceptance criteria and required thread fit
- Quantity by size, packing marks, destination and requested Incoterm
- Material, mechanical, coating and third-party inspection documents
Frequently asked questions
Why was hot-dip galvanizing specified for the Mauritius project?
The buyer's specification described a humid, saline coastal environment. HDG was therefore part of the project fastener specification, together with thread-fit and documentation requirements.
Can one coating thickness be used for every custom fastener order?
No. The applicable standard, fastener size, thread pitch, material, required fit and signed order determine the coating and acceptance criteria.
What is the most important drawing information for an M20 custom bolt?
Confirm overall length, full or partial thread, thread pitch, thread length, head and nut geometry, washer dimensions, tolerances, material class, finish and inspection documents.
Send the drawing, bill of materials, standards, coating requirement, quantity and destination to sales@yyfasteners.com. You can also review our hex bolt range, spring washers, management-system certificates and quotation form.


